Oct Back to list
Precision Bar Level how to replace a toilet fill valve Performance Analysis
Precision in industrial alignment is rarely about the large-scale movements; it is about the micron-level deviations that determine the lifespan of a machine tool. When a technician asks how to replace a toilet fill valve, they are usually dealing with residential plumbing, but in the world of high-end manufacturing, "valves" and "levels" refer to the critical calibration of heavy machinery and fluid control systems.
In the casting and tool-making industry, the ability to detect a tilt as small as 0.02mm/m is the difference between a high-performance CNC spindle and a costly mechanical failure. This requirement for extreme accuracy has led to the development of specialized bar levels, which differ significantly from standard frame levels in both geometry and application.
Understanding the technical nuances of precision measurement allows engineers to optimize equipment setup and ensure structural integrity. This article examines the operational logic of high-precision bar levels and how they serve as the backbone for cylindrical workpiece alignment.
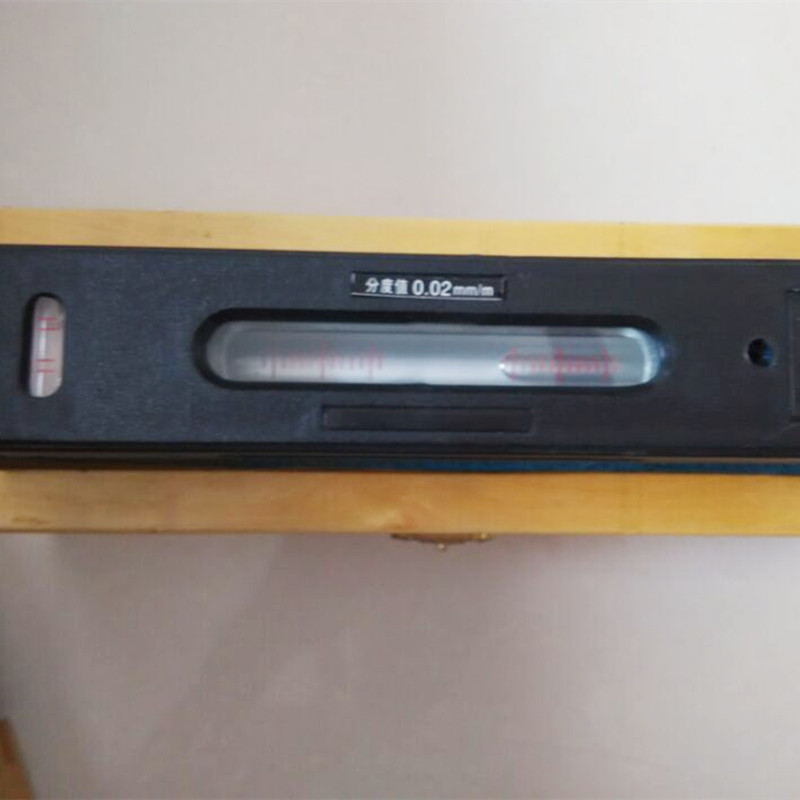
The Mechanics of Linear Precision Measurement
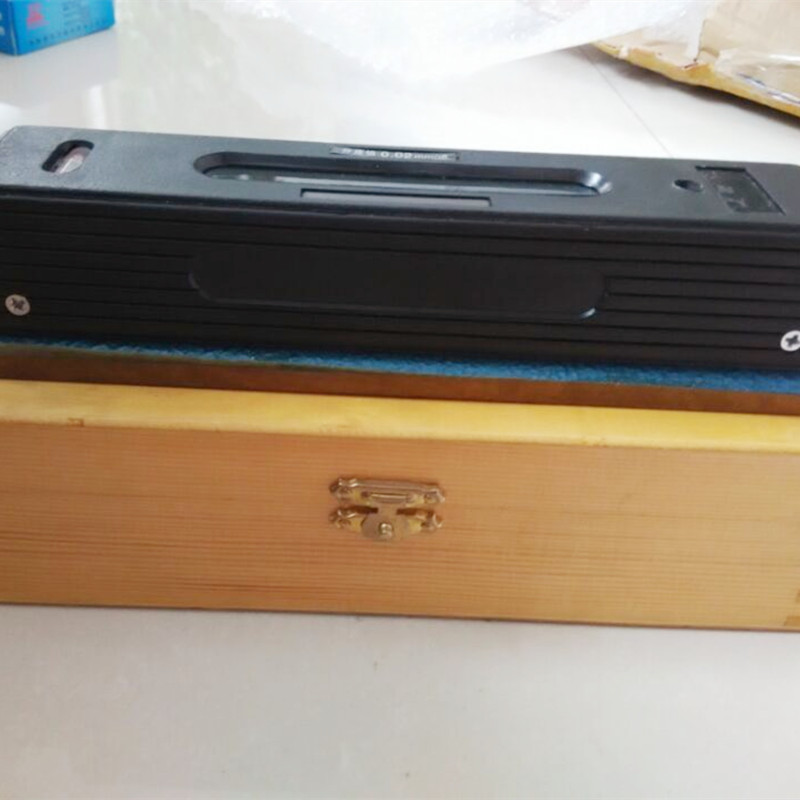
At its core, a bar level is a compact, linear tool designed to measure straightness and inclination on both flat and cylindrical surfaces. Unlike general-purpose levels, industrial bar levels utilize a heat-treated cast iron body to resist deformation and dampen external vibrations, ensuring that the bubble vial provides a stable reading.
The fundamental objective is to detect subtle tilts—often as low as 0.02mm/m—which could otherwise lead to significant runout in machine tool shafts or conveyor rollers. This level of precision is achieved through a combination of optical-grade glass vials and temperature-stabilized fluids.
Technical Design of the V-Grooved Base
The most critical feature of a bar level is its V-grooved base. This geometric design allows the tool to sit securely on cylindrical workpieces, such as pipes or machine shafts, without slipping. The groove is typically ground to micron-level tolerances with a mirror finish (Ra ≤ 0.8μm), creating a stable interface that eliminates measurement inconsistencies.
A 120° angle is standard for these grooves, ensuring that the center of the tool aligns perfectly with the longitudinal axis of the cylinder. This allows the technician to verify the straightness of a shaft across its entire length, which is essential for preventing workpiece defects in aerospace and automotive assembly.
Without this specialized base, measuring round components would require complex jigs or improvised supports, both of which introduce human error and compromise the 0.02mm/m accuracy standard.
Critical Differences: Bar vs. Frame Levels
Selecting between a bar level and a frame level depends entirely on the geometry of the surface being inspected. While both may offer high accuracy, their structural design dictates their application. Frame levels are rectangular and designed for multi-dimensional flatness checks on large, flat planes like machine bases.
Bar levels specialize in single-axis alignment and cylindrical surfaces, offering portability and accessibility in confined spaces where a bulky frame level cannot fit.
In a typical workshop, a frame level is used to ensure a CNC machine is level with the floor, whereas a bar level is used to ensure the internal shafts and guides of that machine are perfectly aligned. This complementary relationship ensures that the entire production line maintains dimensional stability.
Calibration Sensitivity and Accuracy Index
The accuracy of a precision level is measured by its ability to detect deviation over a fixed length. For a tool rated at 0.02mm/m, the bubble vial must be meticulously calibrated using a three-step process to ensure the bubble rests at the center only when the surface is perfectly horizontal.
To maintain this sensitivity, the fluid inside the vial must be temperature-stabilized. Even slight changes in ambient temperature can cause the fluid to expand or contract, potentially shifting the bubble and leading to false readings.
Figure 2. Relative Precision Index by Tool Type
Application in Cylindrical Workpiece Alignment
In high-precision manufacturing, the alignment of CNC spindle shafts is a primary application for bar levels. Even a micro-tilt in the spindle can cause "chatter" during machining, leading to poor surface finish and premature tool wear. By placing a bar level along the shaft's longitudinal axis, technicians can ensure that the spindle is perfectly aligned with the machine's travel path.
Similarly, in the oil and gas sector, the straightness of heavy-duty pipeline segments is verified using bar levels during assembly. This prevents structural stress and flow inefficiencies that occur when pipe segments are slightly misaligned, demonstrating the tool's versatility from the machine shop to the construction site.
Environmental Factors Affecting Measurement
The precision of a bar level is not just a result of its construction, but also how it is used. One of the most significant risks is temperature fluctuation. Because the liquid inside the vial is sensitive to thermal expansion, technicians must avoid direct sunlight and minimize hand contact, which can transfer body heat to the tool.
Surface cleanliness is another critical factor. Any burrs, rust, or dust particles on the measuring surface can lift the V-groove by a few microns, which is enough to invalidate a 0.02mm/m reading. Therefore, a strict cleaning and wiping protocol is required before any measurement begins.
Lastly, parallax error—the distortion caused by viewing the bubble vial from an angle—must be mitigated. Readings should always be taken from a position perpendicular to the vial to ensure that the bubble's center is accurately aligned with the graduation marks.
Selection Framework for Precision Tools
Choosing the right measurement tool requires a clear understanding of the workpiece geometry and the required tolerance. For users focusing on cylindrical components, the bar level is the only logical choice due to its integrated V-groove. For those managing large flat surfaces, the frame level's multi-surface capability is superior.
When evaluating a precision tool, one should look for traceability. A tool that comes with an ISO 17025-certified calibration report ensures that the stated accuracy is not just a nominal value but a verified performance metric.
The following table provides a relative comparison to help engineers decide which tool is most suitable for specific industrial scenarios.
| Scenario | Recommended Tool | Key Technical Factor | Suitability Index |
|---|---|---|---|
| CNC Spindle Alignment | Bar Level | V-Groove Stability | High |
| Machine Bed Flatness | Frame Level | Multi-surface Reference | High |
| Pipeline Straightness | Bar Level | Compact Portability | High |
| Woodworking Tables | Frame Level | Large Plane Stability | Medium |
| Hydraulic Shafts | Bar Level | Cylindrical Fit | High |
| General Construction | Spirit Level | Rough Tolerance | Low |
Questions & Answers
A bar level is specifically designed for the precision measurement of straightness and inclination on linear surfaces, with a particular focus on cylindrical workpieces. Its integrated V-grooved base allows it to lock onto round shafts, making it indispensable for aligning CNC spindles, conveyor rollers, and industrial piping where a standard flat level would slip and produce inaccurate results.
The V-groove creates two points of contact with the cylinder, which automatically centers the tool on the workpiece's longitudinal axis. When ground to micron-level tolerances (Ra ≤ 0.8μm), it eliminates slippage and ensures that the bubble vial is measuring the actual tilt of the shaft rather than an angled or unstable position, maintaining the 0.02mm/m accuracy standard.
Choose a frame level when you need to verify the flatness or squareness of large, flat surfaces. Frame levels feature multiple machined surfaces (top, bottom, sides), allowing for simultaneous horizontal and vertical measurements. Bar levels are preferred for cylindrical parts, narrow rails, or confined spaces where a compact, single-axis tool is required.
Precision levels use temperature-stabilized fluids in their vials. If the tool is exposed to direct sunlight or hand heat, the fluid can expand, which shifts the bubble's position. Even a tiny expansion can lead to a reading error that exceeds the 0.02mm/m tolerance, effectively rendering the precision calibration useless during critical alignment tasks.
ISO 17025 is the international standard for testing and calibration laboratories. A tool with this certification has been verified by a competent body to meet its stated specifications. For an engineer, this means the 0.02mm/m accuracy is a traceable fact, providing the necessary confidence for aerospace or medical equipment manufacturing where tolerances are non-negotiable.
Parallax error occurs when the observer's eye is not perfectly aligned with the center of the vial, making the bubble appear shifted. To eliminate this, always position your line of sight exactly perpendicular to the vial. Reading from a vertical position ensures that you are observing the true center of the bubble relative to the graduation marks.
Final Thoughts
Precision measurement in the casting and tooling industry is an exercise in controlling variables. From the selection of a robust cast iron body to the meticulous grinding of a V-grooved base, every detail is engineered to eliminate error. Whether aligning a CNC spindle or verifying a pipeline, the use of a high-precision bar level ensures that the smallest deviations are detected before they become systemic failures.
As manufacturing moves toward even tighter tolerances, the reliance on traceable, calibrated tools will only increase. By understanding the technical distinctions between bar and frame levels and adhering to strict operational protocols, technicians can ensure that their equipment operates at peak efficiency and longevity.